Case note · Turning and milling · Titanium

Titanium TC4 prototypes held to ±0.05 mm

A research institute needed 30 prototype parts in TC4 titanium: a grooved outside, a pocketed inside, small tapped holes, ±0.05 mm on diameters and hole positions, and Ra 1.6 on the functional faces.

Material
TC4 / Ti-6Al-4V
Quantity
30 pcs
Customer
Research institute
Tolerance
±0.05 mm
Surface
Ra 1.6
Smallest features
M2, Ø1.6 mm holes
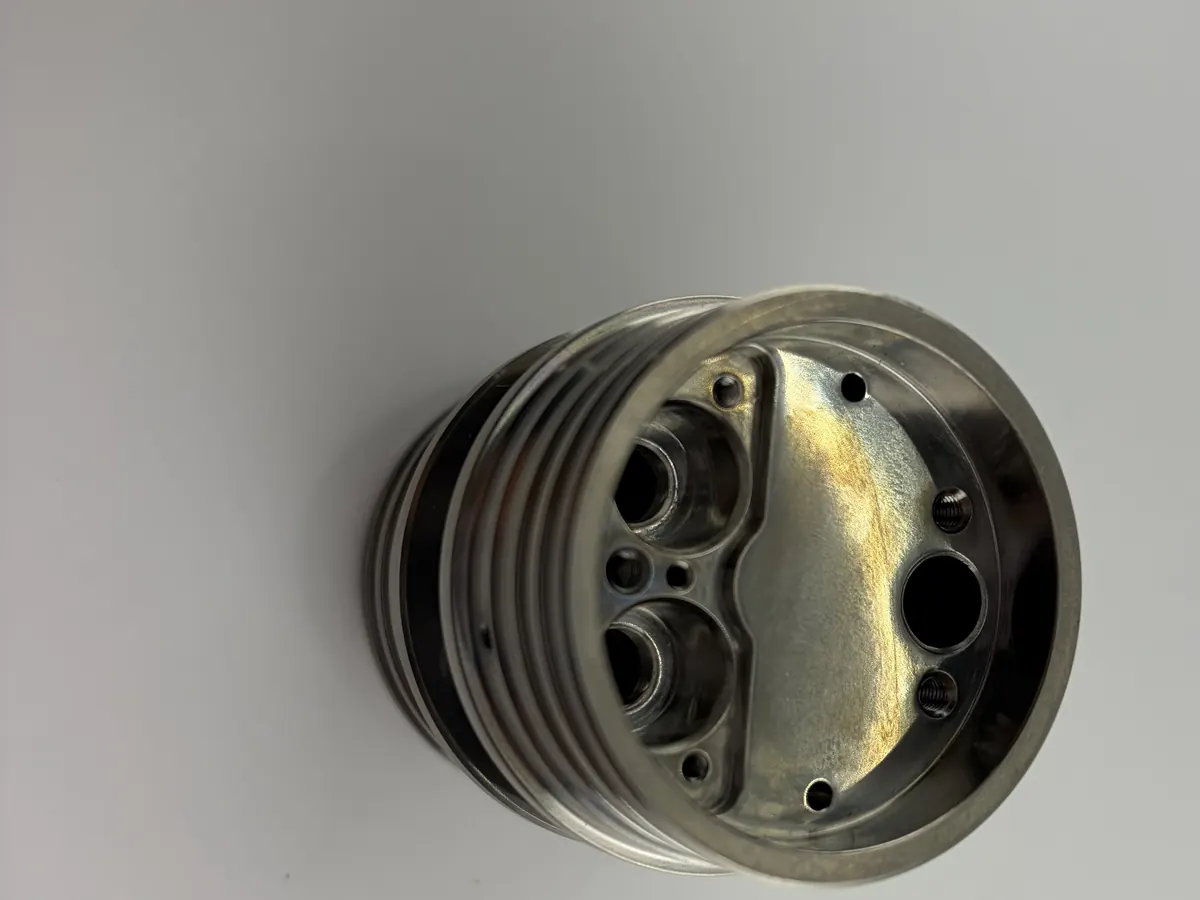
Finished TC4 titanium prototype with internal pockets, bores, and small holes
One of the 30 finished TC4 parts, about Ø45 mm. Drawing and customer details are not shown.
The problem

Why this part was hard to make in titanium

  • Titanium keeps heat at the cutting edge. It conducts heat poorly, so the tool runs hot and wears fast, which moves sizes during a batch.
  • It springs back. Titanium flexes under the tool more than steel, so thin ribs between the grooves can push away and come back oversize.
  • Small threads break taps. M2 and M3 threads and Ø1.6 mm holes in titanium leave little margin before a tap or drill snaps in the part.
  • Many tight features at once. Diameters and hole positions at ±0.05 mm, with untoleranced features to GB/T 1804-f.
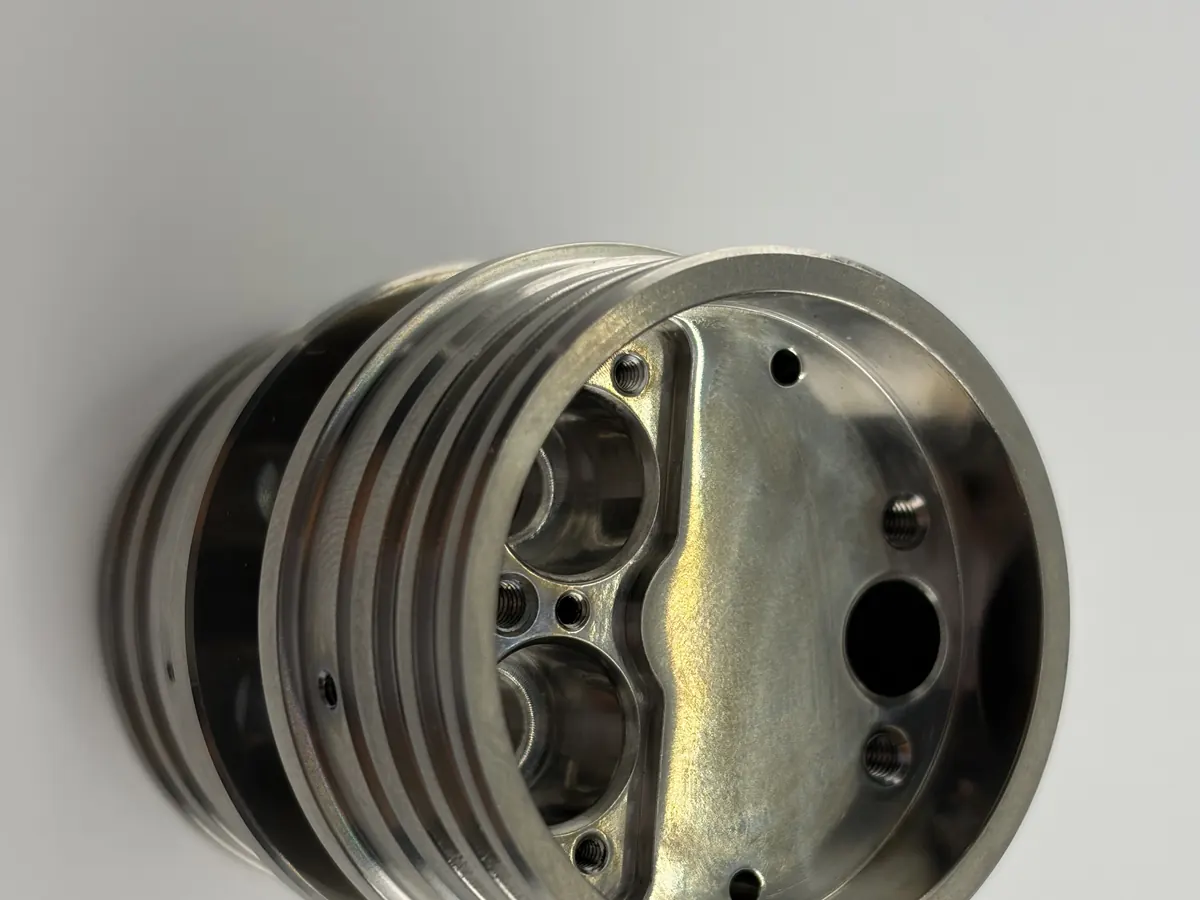
TC4 titanium prototype seen from the side
Internal pockets, bores, and small tapped holes, all tied to the same datum.
What the drawing asked for

Many precision features on one small part

  • ±0.05 mm on the stepped diameters and on the positions of the internal holes.
  • Ra 1.6 on the functional faces; untoleranced features to GB/T 1804-f, the fine class.
  • M2 and M3 threads and Ø1.6 mm holes, some about 7.5 mm deep, all positioned from the same datum.
  • External grooves with thin ribs between them, R0.5 internal corners, C0.5 chamfers, and every edge deburred.

All 30 parts were machined in our Dongguan factory from TC4 bar. Workholding and process photos will be added to this note.

More parts from recent orders → · Thin-wall 304 rings case →

TC4 titanium prototype with external grooves and thin ribs
External grooves with thin ribs between them.
For your drawing

Designing a precision titanium part?

Three things that make titanium parts easier to make and cheaper to quote.

Name the grade

Write TC4 / Ti-6Al-4V, or Grade 2 for commercially pure titanium. The two machine and cost differently.

Keep ±0.05 mm where it matters

Tight tolerances on every feature multiply the time per part. Put them on the fits and positions that work.

Give small threads room

Allow a little extra thread depth or a through hole for M2 and M3 where you can. It lowers the risk of a broken tap in the part.

Have a titanium part with tight tolerances?

Send the drawing. We'll tell you how we would hold and cut it, and quote it with DFM notes. Email reply within 24 hours.

Send Your Drawing